How to compare energy-efficient screw compressors by specific power




Comparing energy-efficient screw compressors requires more than reviewing motor ratings or advertised efficiency figures. Specific power—the electrical input required to deliver a given volume of compressed air—offers a practical basis for evaluating performance, provided measurements use comparable pressure, flow and operating conditions. For engineers searching for air compressors energy efficient enough to reduce lifecycle costs, the challenge is turning a promising datasheet number into a credible estimate of plant energy use.
A compressor that looks excellent at full load may be less convincing when demand falls on a night shift. Another may have a slightly higher quoted specific power but include a dryer and cooling fan that its competitor leaves outside the measurement boundary. Those differences are not footnotes: they can change the purchasing decision.
Start with the ratio, then check what is inside it
Specific power is electrical input divided by delivered air flow, commonly expressed as kW per m³/min or kW per 100 cfm. A lower value means less electrical power is required for the stated air output at the stated conditions. It does not, on its own, tell you how much electricity the compressor will use over a year.
Take a simple illustration: a package drawing 75 kW while delivering 12 m³/min has a specific power of 6.25 kW per m³/min. A second package drawing 80 kW and delivering 13 m³/min has a value of approximately 6.15 kW per m³/min. The second appears more efficient at those points, despite its higher input power. These are illustrative figures, not expected performance benchmarks.
That comparison only holds if both machines deliver air at the same pressure and if their flow and power are measured on equivalent bases. Ask whether the quoted flow is free air delivery, corrected to the stated inlet reference conditions, rather than swept volume or another capacity figure. Swept volume describes displacement; it is not the same as the usable air delivered by the package.
Also establish where electrical input is measured. A motor shaft rating, motor input and complete package input are different quantities. Depending on the configuration, package power can include the drive, cooling fan, oil pump and controls. An integrated dryer or a separate water-cooling system may sit inside or outside that boundary. Neither convention is automatically wrong, but the quotations must make it possible to reconcile the difference.
Make the test conditions comparable
Pressure is usually the first mismatch to resolve. Compressing air to a higher discharge pressure requires more work, so a lower specific-power figure at a lower pressure is not proof of a better compressor. Compare units at the pressure required at the compressor outlet, allowing for realistic losses through dryers, filters, piping and controls. Do not compare a figure measured upstream of treatment with one measured downstream without accounting for that difference.
For a defensible comparison, request the following for each operating point:
- Discharge pressure, including whether it is gauge or absolute, and the measurement location.
- Delivered flow, flow units and inlet reference conditions used to express it.
- Total electrical input and a clear list of included auxiliaries.
- Inlet air temperature, cooling conditions and any corrections applied to the results.
- Test method, tolerances and whether the figures are guaranteed or indicative.
ISO 1217 is a relevant reference for displacement compressor acceptance testing, but citing it is not a substitute for reading the test documentation. Confirm the applicable edition, test arrangement and scope with the supplier. If a project specifies a performance guarantee, agree in advance how flow and power will be measured, corrected and judged during acceptance.
Ambient conditions matter in practice as well as on paper. A hot compressor room or restricted cooling airflow can alter performance and operating margins. Water-cooled packages need a credible cooling-water temperature, flow and pressure-drop assumption. A favorable factory rating at reference conditions may not represent a site with challenging summer conditions.
Compare the load profile, not just the nameplate point
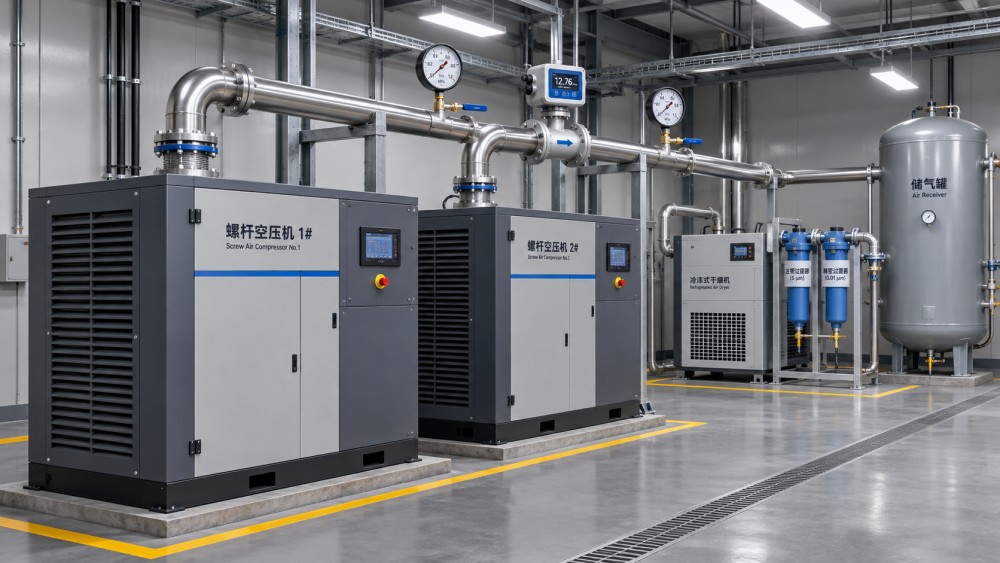
The most useful full-load number is still only one point on a curve. A fixed-speed rotary screw compressor using load/unload control can draw substantial power while unloaded, even though it delivers no useful air during that interval. Receiver storage, pressure band and control settings affect how often it cycles. For a plant with long low-demand periods, unloaded power and time spent unloaded deserve as much attention as the full-load ratio.
A variable-speed drive can match output to changing demand within its operating range, but it is not automatically the lowest-energy choice at every point. Drive losses, minimum stable speed and operation near the top of the range all matter. Below minimum output, the machine may unload, stop or use another control strategy; request the associated power and operating assumptions rather than extending a smooth efficiency curve down to zero flow.
Consider a facility with steady production during the day and a much lighter overnight load. A fixed-speed compressor sized for the peak might be economical during the day but spend much of the night unloaded. A variable-speed unit may handle the transition more effectively, although a smaller trim machine alongside a fixed-speed base-load unit could also be worth evaluating. The right answer depends on the measured demand distribution, required standby capacity and how the machines are sequenced.
If interval data are available, group operating hours into representative demand bands. For each band, estimate package power at the required delivered flow and multiply it by the hours in that band. Add the results to estimate annual electricity consumption. Use a load profile measured across normal shifts, weekends and seasonal changes where possible; a single busy-day snapshot can make an oversized machine look appropriate.
For multiple compressors, model the station rather than ranking individual machines in isolation. Include base-load and trim assignments, pressure setpoints, unloaded running and standby requirements. A machine with the best standalone rating can still be a poor fit if its capacity leaves the trim compressor operating inefficiently or forces unnecessary pressure cycling.
Put the whole air system on the same boundary
Compressor selection begins with the air users. Determine the minimum pressure and air quality actually required at critical points of use, then work back through the treatment equipment and distribution network. Raising the station pressure to compensate for undersized filters or a restrictive pipe can hide a system problem and increase compression work across the installation.
Dryers and filters introduce their own trade-offs. A lower pressure-drop treatment train may reduce the pressure the compressor must produce, but dryer electricity, purge air where applicable, maintenance and required dew point must also be considered. If one proposal includes an integrated dryer and another relies on a separate dryer, compare the complete combinations at the same delivery point and air quality.
Oil-injected and oil-free screw compressors should likewise be evaluated against the process requirement, not reduced to a single efficiency claim. Oil-free production may be justified by contamination risk or process specifications; oil-injected designs rely on appropriate separation and downstream treatment. The cost and energy boundary should include the treatment, monitoring and maintenance needed to meet the required air quality in each proposal.
Leaks and inappropriate uses complicate sizing. A compressor must initially support the load that exists, but using an unrepaired leak load as a permanent design target can lock in excess capacity. Where practical, quantify leakage and identify planned corrective work before fixing the duty point. Keep a separate allowance for credible future demand rather than burying an unexplained safety margin in every assumption.
Turn the comparison into an annual cost decision
Once expected annual kWh has been estimated, apply the relevant electricity charges. A flat energy rate may be sufficient for screening, but a final financial model may need time-of-use prices, demand charges or other site-specific tariff components. Compare purchase price and installation costs alongside service intervals, consumables, cooling requirements and expected downtime arrangements. State the analysis period and discounting assumptions so that proposals can be challenged on the same basis.
Heat recovery can affect the economics, but recovered heat should not be treated as free credit simply because a compressor produces it. Check that there is a coincident heat demand, a useful temperature, a suitable heat exchanger and an operating plan for periods when the heat cannot be used. Account for installation and any additional pumping power. Keep gross electrical consumption visible even when reporting net energy benefits.
The Global Thermal & Compression Matrix takes this connected view of compression and thermal systems: the efficiency of a package matters, but so do cooling conditions, heat use and the economics around it. For technical evaluation, that perspective is most useful when it leads to a transparent calculation rather than a single headline number.
What to request before placing an order
Ask shortlisted suppliers for power and delivered flow at the project pressure across the expected operating range, including unloaded and minimum-output behavior. Request the measurement boundary, reference conditions, auxiliary loads, tolerances and control sequence. Where a curve is unavailable, identify the missing points as an uncertainty in the cost model rather than assuming the quoted full-load ratio applies all year.
Finally, agree on an acceptance method that reflects the installed system and can distinguish compressor performance from site restrictions. The best choice is the package—or combination of packages—that meets pressure and air-quality requirements with the lowest credible lifecycle cost under the plant’s actual load profile. If two bids are close, the quality of the supporting data and the service arrangements may be more decisive than a small difference in advertised specific power.
Ready when you are. Send us a message to get started.
Related News
- How to compare energy-efficient screw compressors by specific powerAuthor :Pneumatic Power Engineer

- How to tell when compressed air filter elements need replacingAuthor :Pneumatic Power Engineer

- How to compare compressor flow ratings using free air deliveryAuthor :Pneumatic Power Engineer

- When does variable gas flow justify a custom screw compressor system?Author :Pneumatic Power Engineer

- How to size compressed air equipment for pneumatic toolsAuthor :Pneumatic Power Engineer

- How Should Energy Management Systems Handle Compressor Load Changes?Author :Pneumatic Power Engineer

- Which Maintenance Issues Reduce Air Compressor Efficiency?Author :Pneumatic Power Engineer

- How Much Energy Can Variable-Speed Screw Compressors Save?Author :Pneumatic Power Engineer

- Industrial Compressor Selection: Matching Flow, Pressure, and Duty CycleAuthor :Pneumatic Power Engineer

- China Expands Cross-Border RMB and FX Cash Pooling NationwideAuthor :Pneumatic Power Engineer

- How to Size Air Compressor Systems for Pneumatics by Flow and Pressure DemandAuthor :Pneumatic Power Engineer

- How Energy Recovery Systems for Compressors Cut Power CostsAuthor :Pneumatic Power Engineer

- How to Evaluate Screw Compressors in Industrial Refrigeration EquipmentAuthor :Pneumatic Power Engineer

- India Makes BIS Certification Mandatory for Screw CompressorsAuthor :Pneumatic Power Engineer

- China Tightens Export Filing for Screw CompressorsAuthor :Pneumatic Power Engineer

- SABIC Sets IoT Interface Rule for Screw CompressorsAuthor :Pneumatic Power Engineer

- Industrial Heat Recovery Systems for Compressors: When Do Energy Savings Pay Back?Author :Pneumatic Power Engineer

- EU Tightens REACH Limit for Screw Compressor LubricantsAuthor :Pneumatic Power Engineer

- EU Opens China Screw Compressor Review With Carbon RuleAuthor :Pneumatic Power Engineer

- DOE Mandates AHRI 1000-2026 for Screw CompressorsAuthor :Pneumatic Power Engineer

- VDMA Filing Signals EU Risk for Chinese Oil Screw CompressorsAuthor :Pneumatic Power Engineer
![]()
- Screw vs Piston Air Compressors for Stable Plant OutputAuthor :Pneumatic Power Engineer

- Saudi SASO Tightens Refrigerant Limits in IEC 60335-2-40:2026Author :Pneumatic Power Engineer

- IIR Warns of 18-Week Lead Times for Screw CompressorsAuthor :Pneumatic Power Engineer

- Welded Compressed Air Manifold Selection Guide for Pressure Stability and LeaksAuthor :Pneumatic Power Engineer

- India BIS Rule Adds IS 16830 Requirement for Imported Screw CompressorsAuthor :Pneumatic Power Engineer

- What to Check Before Choosing a Compressed Air FactoryAuthor :Pneumatic Power Engineer

- China Tightens Export Checks on Screw CompressorsAuthor :Pneumatic Power Engineer

- Screw Compressor Lead Times Reach 22 WeeksAuthor :Pneumatic Power Engineer

- Vietnam Requires QR Labels on Imported Screw CompressorsAuthor :Pneumatic Power Engineer

- Compressed Air Technologies Filtration: How to Reduce Pressure Drop and Energy LossAuthor :Pneumatic Power Engineer

- STSPIN830 Lead Time Tops 32 Weeks in Screw CompressorsAuthor :Pneumatic Power Engineer

- IGBT Shortage Extends Screw Compressor Lead TimesAuthor :Pneumatic Power Engineer

- Compressed Air Systems: 7 Hidden Costs That Raise Total Operating ExpenseAuthor :Pneumatic Power Engineer

- Compressed Air Efficiency: 7 Hidden Losses That Raise Operating CostsAuthor :Pneumatic Power Engineer

- How to Compare Screw vs Oil-Free Air Compression SystemsAuthor :Pneumatic Power Engineer